소개:
Aluminum laser welding is transforming modern manufacturing with precision, speed, and consistency that traditional arc welding cannot match. From automotive battery trays to aerospace components, it has become the preferred method for high-volume production where quality and repeatability are critical. Although aluminum’s reflectivity, conductivity, and oxide layer make it challenging for conventional welding, these properties suit laser technology well when properly controlled. This guide answers key questions: What is laser welding? How does it compare to TIG and MIG? Are laser welds as strong as arc welds? And how thick can a laser welder weld? Whether you are evaluating this technology for production or exploring its fit for your application, this article provides the practical knowledge you need.
What Is Laser Welding?
Understanding what laser welding is provides the foundation for appreciating its role in aluminum fabrication. Laser welding is a high-energy-density fusion welding process that uses a focused beam of coherent light to melt and join metal workpieces. The word “laser” stands for Light Amplification by Stimulated Emission of Radiation, and in industrial welding, this concentrated light beam is generated by a laser source, delivered through fiber optic cables or mirrors, and focused onto the workpiece using precision optics.
The key characteristic of laser welding is its extremely high power density. A typical industrial laser can focus several kilowatts of power onto a spot measuring just 0.1 to 0.6 mm in diameter, producing power densities exceeding one million watts per square centimeter. This intense concentration of energy causes the metal to melt and, in deep-penetration mode, vaporize, creating a narrow vapor cavity known as a “keyhole.” The keyhole allows the laser beam to penetrate deeply into the material, producing narrow, deep welds with minimal heat input to the surrounding material.
For aluminum laser welding specifically, the process offers several distinct advantages. The concentrated heat source produces a narrow heat-affected zone, which is particularly valuable for heat-treated aluminum alloys that lose strength when exposed to prolonged elevated temperatures. The rapid heating and cooling cycles also produce fine grain structures in the weld metal, often resulting in excellent mechanical properties. Additionally, the non-contact nature of laser welding eliminates electrode wear, reduces contamination, and allows for welding in locations that are difficult to access with traditional torches.
The main types of lasers used for aluminum laser welding include fiber lasers, disk lasers, and Nd:YAG lasers. Fiber lasers have become the dominant technology in recent years due to their high electrical efficiency, excellent beam quality, low maintenance requirements, and compact size. These lasers operate at wavelengths around 1 micron, which aluminum absorbs relatively well compared to the 10.6-micron wavelength of CO₂ lasers, making fiber lasers far more suitable for aluminum laser welding applications.
Which Is Better for Welding Aluminum: Laser Welding or TIG Welding?
The question of whether laser welding or TIG welding is better for aluminum is one of the most common inquiries in the industry, and the honest answer is that it depends entirely on your production requirements, part geometry, and quality standards. Both processes are capable of producing excellent aluminum welds, but they excel in different scenarios.
TIG welding (Gas Tungsten Arc Welding) has long been the gold standard for manual aluminum welding. Its key advantage is the use of alternating current, which provides a cleaning action that breaks up the aluminum oxide layer during welding. This means TIG can weld aluminum that has not been perfectly cleaned, and it offers the operator real-time control over heat input through a foot pedal or torch-mounted amperage control. TIG welding is ideal for thin aluminum sections, complex geometries, repair work, and applications where weld appearance is critical. It produces clean, spatter-free welds with excellent aesthetic quality.
However, TIG welding is slow. Travel speeds for manual TIG on aluminum typically range from 100 to 250 mm per minute, and the process requires a highly skilled operator whose performance can vary from part to part. For production environments, this variability and slow speed become significant limitations.
Laser welding, by contrast, offers dramatically higher speeds. Aluminum laser welding can achieve travel speeds of 3,000 to 10,000 mm per minute or more—ten to fifty times faster than manual TIG. The process is fully automatable, producing identical welds on every part with no operator fatigue or inconsistency. The narrow heat-affected zone of aluminum laser welding also means less distortion and less loss of temper in heat-treated alloys, which is a major advantage for thin aluminum components.
The trade-off is that laser welding requires extremely tight joint fit-up—typically gaps under 0.1 to 0.2 mm—because the focused beam cannot bridge gaps the way a TIG arc can. Laser welding also has higher equipment costs and requires careful management of aluminum’s high reflectivity and oxide layer.
So which is better? For low-volume, high-mix production, repair work, or parts with complex geometry and poor fit-up, TIG welding remains the more practical and flexible choice for aluminum. For high-volume production of consistent parts with tight tolerances—such as automotive battery components, electronic housings, or thin-walled enclosures—aluminum laser welding is significantly better in terms of speed, consistency, and cost per part. Many manufacturers use both: laser welding for production runs and TIG welding for prototypes, repairs, and rework.
Is Laser Welding as Strong as MIG?
Strength is a critical consideration when selecting a welding process, and the question of whether laser welding is as strong as MIG welding is a common one. The answer is that laser welding can achieve strength comparable to or even exceeding MIG welding, but the relationship is not simple.
MIG welding (Gas Metal Arc Welding) uses a continuously fed filler wire and an external shielding gas. For aluminum, MIG welding is typically performed with a spool gun or push-pull wire feeder and pulsed spray transfer to manage heat input. MIG welds on aluminum generally exhibit good strength, with joint efficiencies typically ranging from 60% to 90% of the base material strength, depending on alloy, filler selection, and weld quality.
Laser welding of aluminum can be performed autogenously (without filler) or with filler wire. Autogenous laser welds derive their strength entirely from the base material, and when full penetration is achieved, the joint efficiency can approach 100% of the base metal strength. With filler wire addition, laser welding can achieve strength levels comparable to MIG welding while maintaining the narrow heat-affected zone and fine grain structure that laser processing provides.
In practice, the strength of aluminum laser welding compared to MIG depends on several factors. Laser welds typically have lower porosity than MIG welds because the rapid solidification and keyhole dynamics help expel gas bubbles, resulting in denser weld metal. Laser welds also have a much narrower heat-affected zone, which means less softening of the surrounding material in heat-treated alloys—an advantage for 6xxx and 7xxx series aluminum. On the other hand, MIG welding with appropriate filler selection can compensate for base metal deficiencies or alloy incompatibilities that autogenous laser welding cannot address.
For fatigue-critical applications, laser welds often outperform MIG welds due to their smooth profile, minimal undercut, and reduced stress concentration. For applications requiring maximum tensile strength in thick sections, MIG with proper filler and full penetration can match laser welding. The consensus in the industry is that laser welding is at least as strong as MIG welding when properly executed, and often stronger in specific applications involving thin sections, heat-treated alloys, or fatigue loading.
Are Laser Welds as Strong as TIG Welds?
The comparison between laser welds and TIG welds follows a similar logic to the laser-versus-MIG comparison. TIG welding is renowned for producing high-quality, strong welds on aluminum, particularly when executed by a skilled operator. A properly executed TIG weld on aluminum can achieve joint efficiencies of 80% to 95% of the base material strength, with excellent ductility and toughness.
Aluminum laser welding, when properly parameterized and with appropriate joint preparation, can achieve strength levels that match or exceed TIG welds. The key advantages of laser welding in this comparison are the narrower heat-affected zone and the finer grain structure of the weld metal. In heat-treated aluminum alloys such as 6061-T6 and 7075-T6, the broad heat-affected zone of TIG welding can cause significant over-aging and strength loss in the region adjacent to the weld. Laser welding’s concentrated heat source minimizes this effect, preserving more of the base material’s mechanical properties.
However, TIG welding has advantages that can translate to higher strength in certain scenarios. TIG allows for precise control of filler metal addition, which can be used to optimize weld chemistry, compensate for fit-up gaps, and tailor the weld bead profile to reduce stress concentration. TIG also allows the operator to adjust heat input in real time, which is valuable for complex parts with varying thickness. In contrast, laser welding requires near-perfect fit-up and consistent material conditions to achieve optimal strength.
Research and industrial experience generally indicate that laser welds on aluminum are at least as strong as TIG welds, provided the joint is properly designed and the process parameters are optimized. In thin-section aluminum, laser welding often produces stronger joints than TIG because of reduced distortion and a narrower heat-affected zone. In thick-section aluminum where full penetration is required, both processes can achieve equivalent strength when properly executed. The choice between them should therefore be driven by production volume, joint geometry, and quality requirements rather than strength alone.
How Thick Will a Laser Welder Weld?
Understanding the thickness capabilities of aluminum laser welding is essential for determining whether the process suits your application. Unlike arc welding, where thickness capability is primarily determined by amperage, laser welding thickness capability depends on laser power, beam quality, focal spot size, welding speed, and the specific aluminum alloy being welded.
For aluminum laser welding, the practical thickness ranges are as follows:
Low-power lasers (500W to 1kW): These systems are suitable for thin aluminum sections ranging from 0.2 mm to 2 mm. Typical applications include electronic component housings, thin-walled battery cell connectors, sensor packages, and foil-to-foil joining. The low heat input of these systems is ideal for delicate aluminum parts where distortion must be minimized.
Medium-power lasers (1kW to 4kW): This is the most common power range for industrial aluminum laser welding. These systems can weld aluminum from 1 mm to 6 mm in single-pass, full-penetration mode, depending on alloy and joint configuration. Applications include automotive battery trays, heat exchanger components, motor housings, and structural brackets. With optimized parameters, a 3kW fiber laser can achieve full penetration on 4 mm to 5 mm aluminum in a single pass.
High-power lasers (4kW to 10kW+): These systems extend the thickness capability of aluminum laser welding up to 10 mm to 15 mm in single-pass welds. They are used for heavy-duty structural components, thick-walled enclosures, and applications in shipbuilding and rail transport. For thicknesses beyond 15 mm, multi-pass laser welding or hybrid laser-arc processes are typically employed.
It is important to note that these thickness ranges are guidelines rather than absolute limits. Aluminum’s high thermal conductivity means heat dissipates quickly from the weld zone, which can limit penetration in thicker sections. The high reflectivity of aluminum also means that a portion of the laser energy is reflected away rather than absorbed, requiring higher nominal power to achieve the desired penetration. For these reasons, aluminum laser welding typically requires somewhat higher power levels than steel laser welding of equivalent thickness.
Joint configuration also plays a significant role. Butt joints with square edges allow the deepest penetration for a given laser power, while lap joints and T-joints may require different parameter settings or filler wire addition to achieve proper fusion. For very thick aluminum sections, hybrid laser-MIG welding—which combines a laser beam with a MIG arc in a single process—can achieve penetration depths of 20 mm to 30 mm while benefiting from the filler metal addition and gap-bridging capability of the MIG arc.
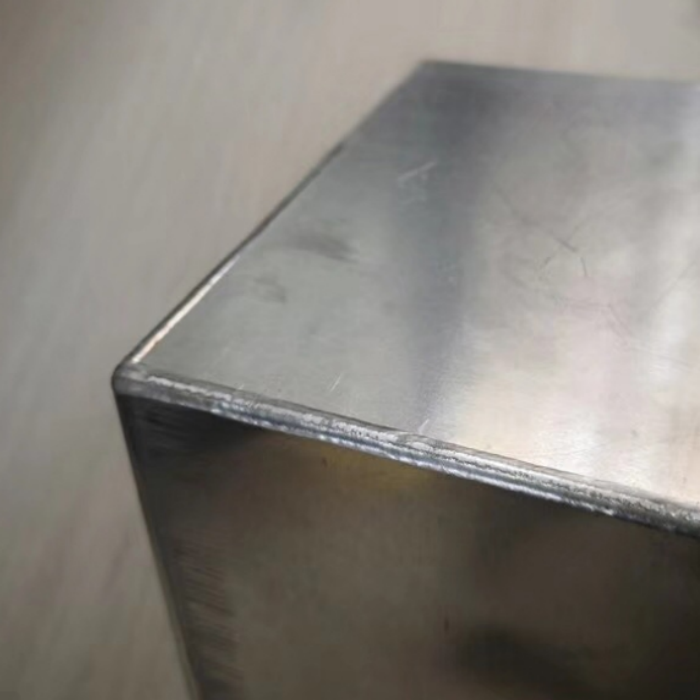
Key Considerations for Successful Aluminum Laser Welding:
Achieving consistent, high-quality results in aluminum laser welding requires attention to several critical factors that differ from steel welding.
Surface preparation and oxide management: Aluminum forms a tenacious oxide layer that melts at approximately 2,000°C, far above the base metal’s melting point of 660°C. This oxide layer must be removed mechanically or chemically before aluminum laser welding, as it can cause incomplete fusion, porosity, and inconsistent penetration. Use a stainless-steel wire brush dedicated exclusively to aluminum, or employ chemical etching. Clean the joint immediately before welding, as the oxide layer reforms within hours.
High reflectivity management: Aluminum reflects a significant portion of incident laser radiation, particularly at the 1-micron wavelength used by fiber lasers. This reflectivity decreases as the material heats and the keyhole forms, but it still requires higher laser power than steel welding. Additionally, reflected laser light can damage optical components, so proper beam delivery design and shielding are essential.
Shielding gas: Aluminum laser welding requires adequate inert gas shielding to prevent oxidation and porosity. Argon is the most common shielding gas, though helium or argon-helium mixtures may be used for higher speed welding or deeper penetration. Gas delivery must be carefully designed to avoid turbulence and ensure complete coverage of the weld pool.
Joint fit-up: Laser welding demands extremely tight fit-up—typically gaps under 0.1 mm for autogenous welding. Any gap larger than the focused beam diameter will result in incomplete fusion or burn-through. This requires precision part fabrication, robust fixturing, and often the use of filler wire to bridge minor gaps.
Filler wire selection: When filler is used in aluminum laser welding, common choices include ER4043 and ER5356. ER4043 offers good fluidity and crack resistance, making it suitable for 6xxx series alloys. ER5356 provides higher strength and better corrosion resistance, making it appropriate for 5xxx and 7xxx series alloys and marine applications.
기공 제어: Aluminum’s rapid solidification in laser welding can trap hydrogen gas, creating porosity. Sources of hydrogen include moisture on the material surface, lubricants, and shielding gas impurities. Thorough cleaning, proper gas purity (99.999% or better), and optimized welding parameters are essential to minimize porosity.
Process monitoring: For production aluminum laser welding, real-time process monitoring systems—including weld penetration monitoring, seam tracking, and plasma detection—are highly recommended to ensure consistent quality and detect defects as they occur.
결론:
Aluminum laser welding is a precise, fast, and consistent process for joining aluminum, outperforming traditional arc welding in many applications. Compared with TIG welding, TIG is better for low-volume, complex, or repair work, while laser welding excels in high-volume production of thin to medium-thickness parts. Its strength is at least equal to MIG welding and comparable to TIG welding, with advantages in heat-treated and fatigue-critical applications due to a narrow heat-affected zone and fine grain structure.
Laser welding can handle thicknesses from 0.2 mm to 15 mm, and hybrid laser-arc processes extend this further. By managing aluminum’s oxide layer, reflectivity, thermal conductivity, and porosity risk, manufacturers can achieve higher quality, greater productivity, and lower cost per part. As technology advances and equipment costs fall, aluminum laser welding is likely to become even more widely used.